

In modern industrial manufacturing and R&D, product reliability is one of the core factors determining market success. Whether in aerospace, automotive electronics, communications equipment, or new energy and advanced materials industries, the stability and durability of products under extreme temperature conditions are critical. As key equipment for simulating harsh temperature environments, high-low temperature test chambers serve as a solid foundation for companies to verify the ultimate performance of their products and enhance their core competitiveness.
I. Handling Extreme Temperature Differences with Precision Simulation of Real-World Challenges
In natural environments and operational conditions, products may face drastic temperature changes—from scorching deserts to frigid zones, from instantaneous startup to prolonged operation. These conditions can lead to material aging, component failure, performance degradation, or even functional breakdown. High-low temperature test chambers precisely control internal temperatures (typically ranging from -70°C to +150°C or beyond) to simulate rapid temperature cycling, constant high/low temperature exposure, and thermal cycling scenarios. This allows potential defects to be exposed early in the R&D phase, providing a scientific basis for design improvements, material selection, and process optimization.
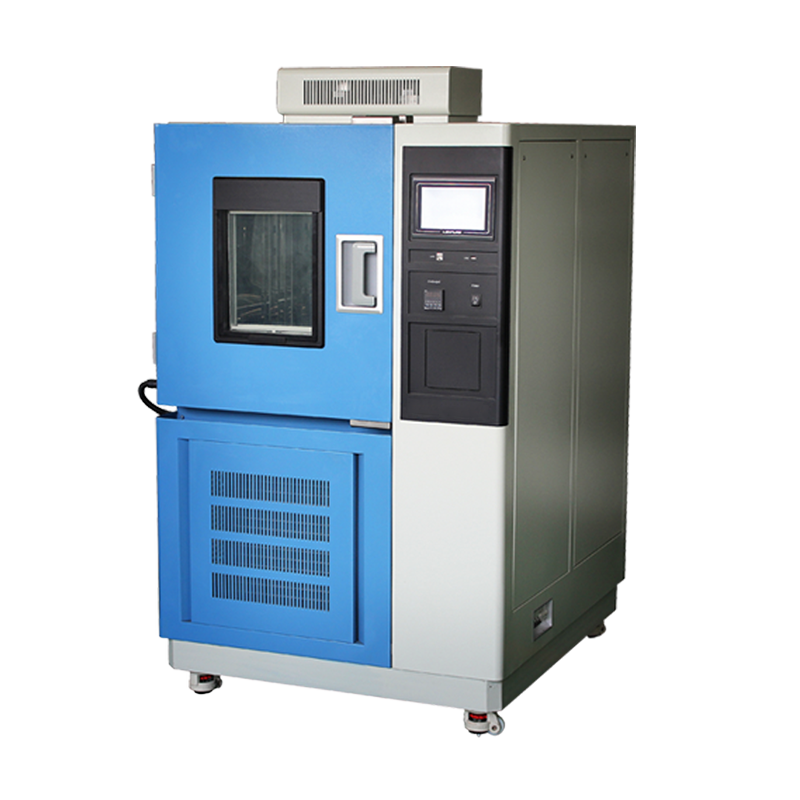
II. Technical Excellence Ensures Authoritative and Reliable Test Data
A high-performance high-low temperature test chamber relies on solid technical foundations and manufacturing craftsmanship. Quality equipment typically features:
-
Precise temperature control systems: Advanced control algorithms and high-sensitivity sensors ensure uniform and stable internal temperatures with minimal deviation and excellent data reproducibility.
-
Efficient cooling/heating design: Rapid achievement of target temperatures with energy-efficient operation, meeting the demands of long-term continuous testing.
-
Robust construction and materials: Stainless steel interiors for corrosion resistance and easy cleaning; insulation thickness and materials balanced for energy consumption and efficiency.
-
Comprehensive safety protections: Over-temperature protection, fault alarms, power interruption recovery strategies, and other functions ensure safe and controllable testing processes.
These features collectively guarantee the accuracy and comparability of test results, providing strong support for companies seeking ISO, GB/T, MIL, and other domestic and international standard certifications.
III. Empowering Industrial Upgrades and Highlighting Customer Value
Introducing high-low temperature test chambers is not merely about meeting basic quality inspection requirements—it represents a forward-looking investment in R&D. It helps customers:
-
Shorten R&D cycles: Simulate years of outdoor environmental effects in the laboratory, accelerating product maturity.
-
Reduce after-sales risks: Identify hidden issues early, minimize field failures, and protect brand reputation.
-
Lower production costs: Avoid massive recall or repair losses caused by batch quality problems.
IV. Choosing a Professional Partner to Safeguard Product Quality
Given the diverse range of equipment models and suppliers on the market, selecting a technically mature and experienced test chamber manufacturer is crucial. An excellent supplier not only provides standard-compliant equipment but also offers customized testing solutions based on actual customer needs, along with one-stop services including installation, training, and maintenance—becoming a long-term partner in enhancing product reliability.
High-low temperature test chambers are essential tools for ensuring products maintain high reliability under drastic temperature changes. Investing in rigorous environmental testing means investing in future market trust and development potential. Let us work together to build more outstanding products that withstand the test of time and environment through reliable technology and equipment.